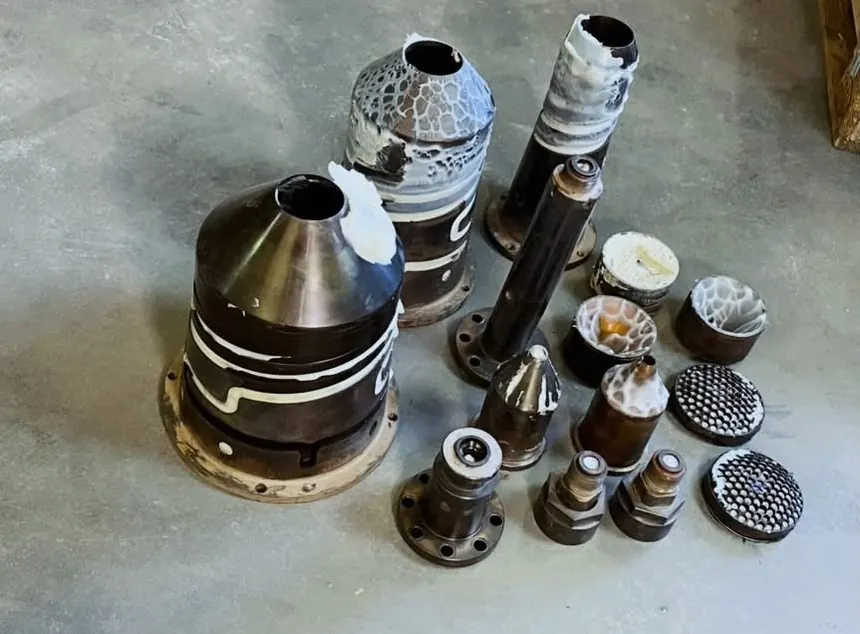
Screws & barrel components
Extruder screws, mixing sections, screw tips, torpedoes and breaker plates. Long screws go in whole, up to the length of the chamber.
Pyrolysis cleaning · Midlands & North West
Pyrolysis cleaning at Arena Comet UK near Stoke-on-Trent. A 5 m × 2 m × 2 m oven chamber takes the extrusion tooling that doesn't fit a standard cleaning oven, and the polymer comes off without scraping, cutting or burning off by hand.
Polymer removed thermally, not mechanically
Long and wide parts in one piece
Collection & return can be arranged
Quote from a photo and dimensions
What we clean
Polymer build-up, degraded material, paint and coatings are removed from steel and other heat-resistant metal parts. Typical work for plastics processors:
Extruder screws, mixing sections, screw tips, torpedoes and breaker plates. Long screws go in whole, up to the length of the chamber.
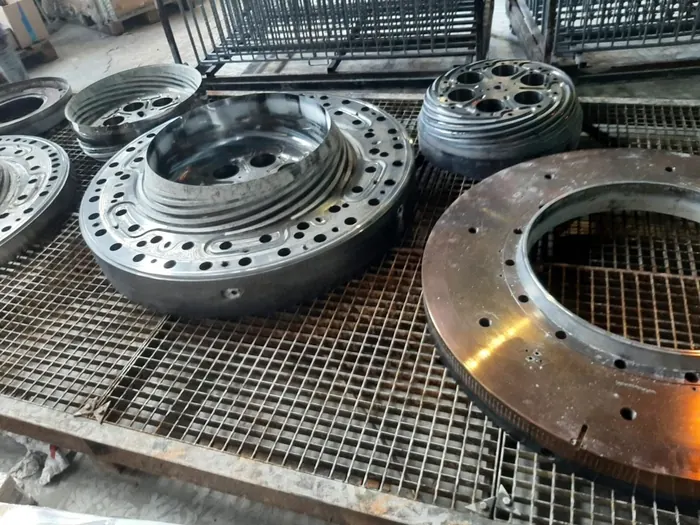
Pipe and profile dies, flat sheet and film dies, coat-hanger dies, die plates and mandrels. Wide dies cleaned without splitting them into sections first.
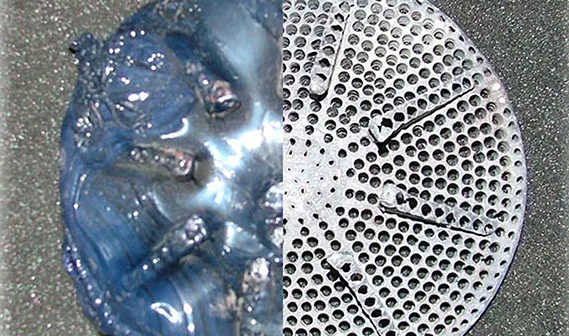
Spinneret plates, spin pack components and spin beam parts for fibre and monofilament lines. Every capillary open again.
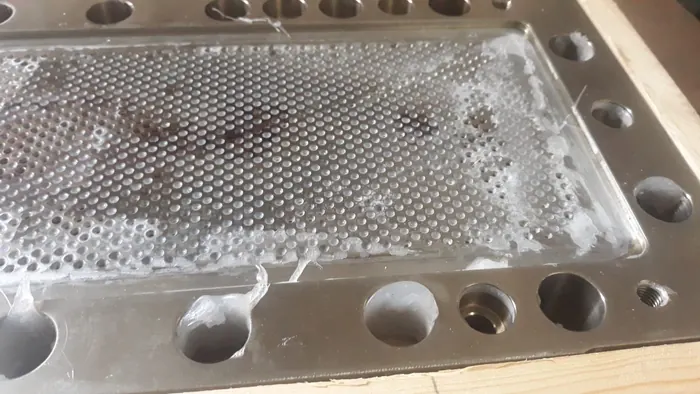
Candle filters, leaf and disc filters, screen changer plates and breaker plates. Polymer is removed from inside the filter media, not just the surface.
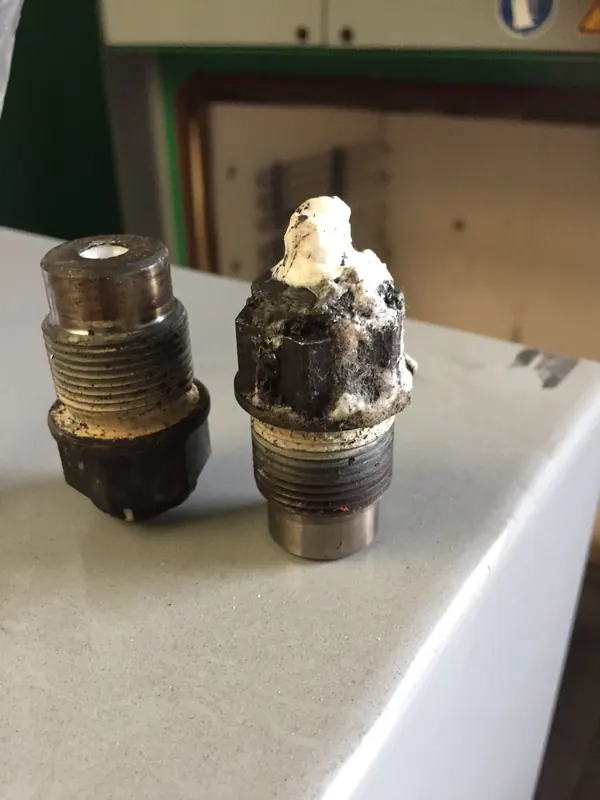
Hot runner nozzles, manifolds and injection moulding parts. Tell us about heaters, thermocouples or seals so we can advise first.
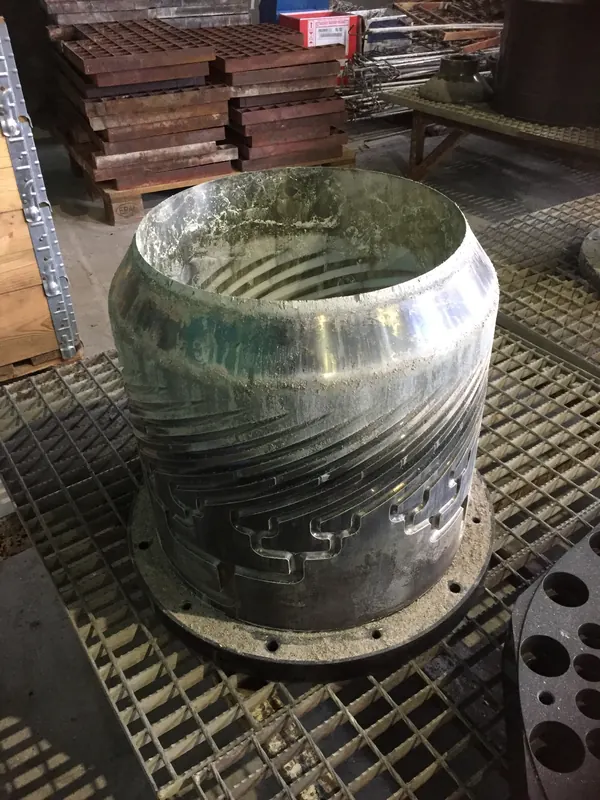
Parison heads, accumulator heads and spiral mandrel distributors with their complex internal channels.
Static mixer elements and housings, adapters, gear pump parts and melt pipes, where polymer degrades in dead spots.
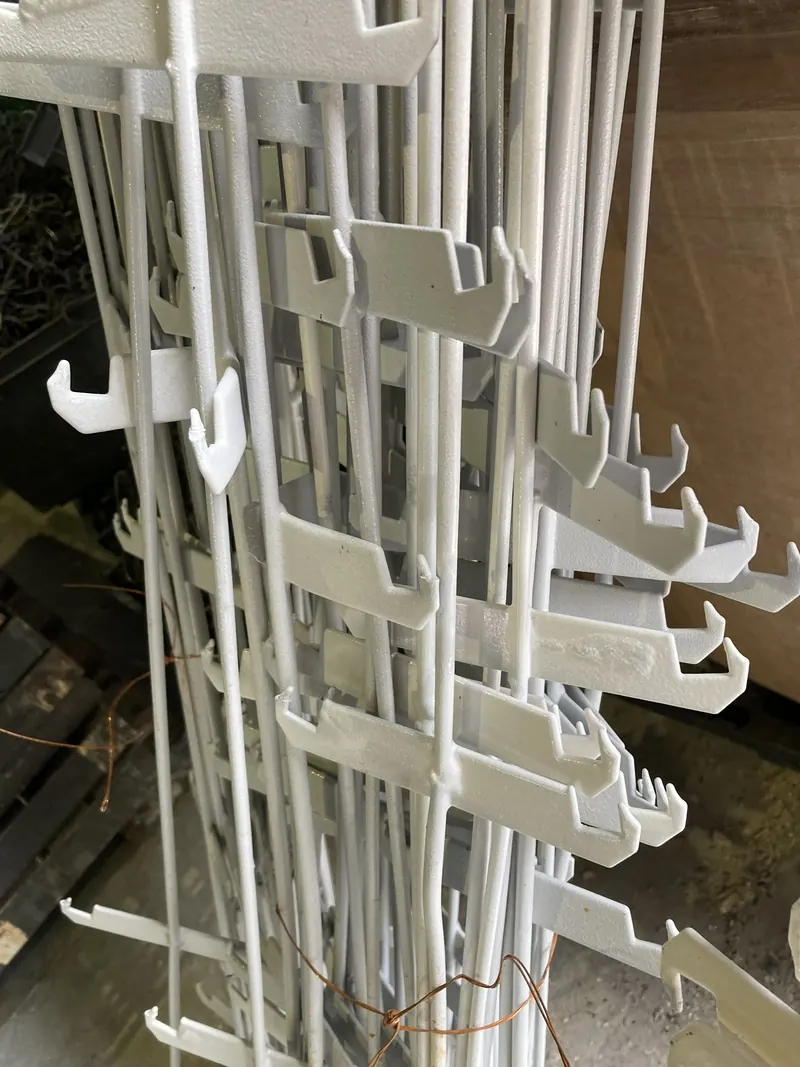
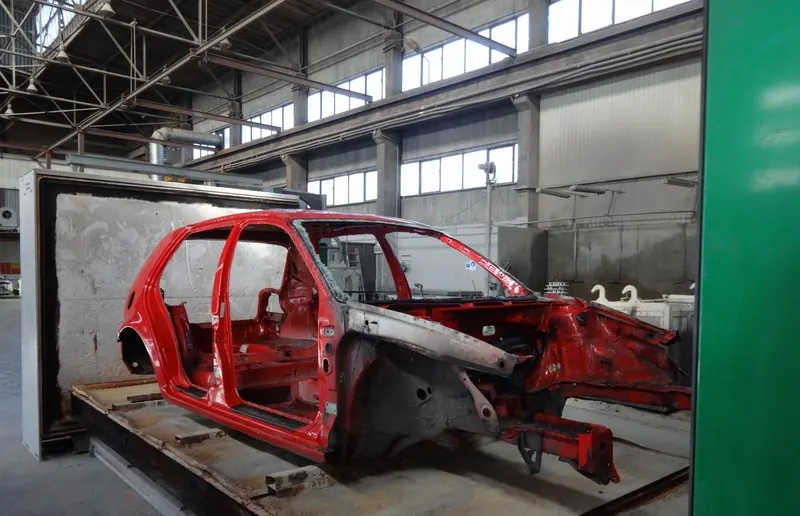
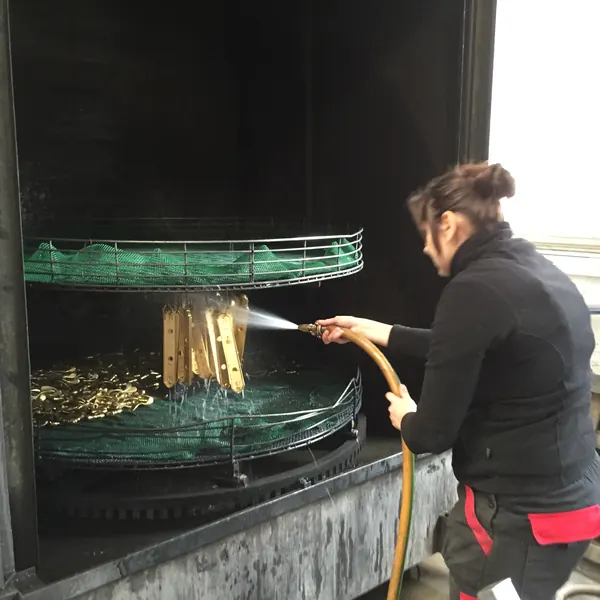
Paint and powder coating build-up removed from racks, jigs, hooks and hangers, so they make good earth contact again.
Before & after
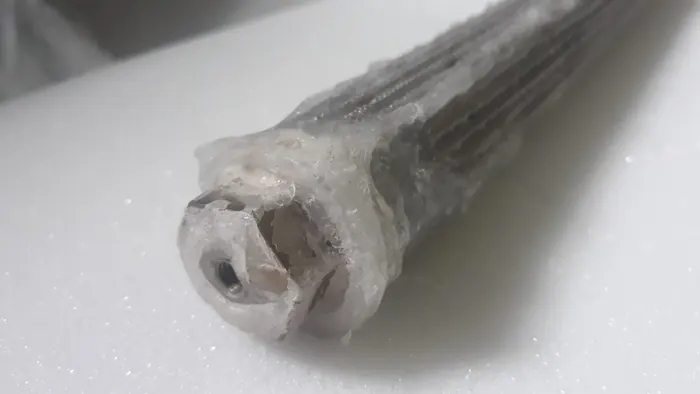
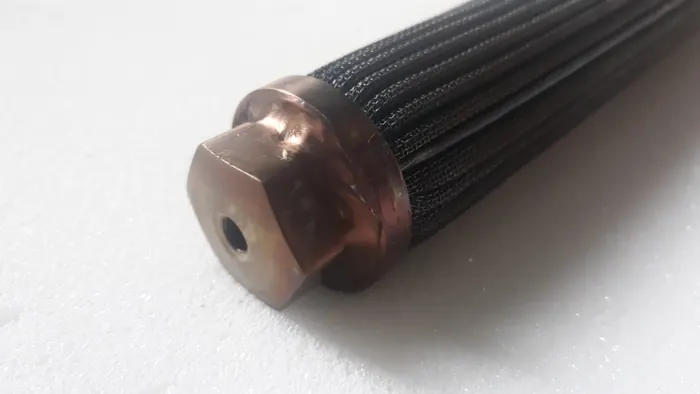
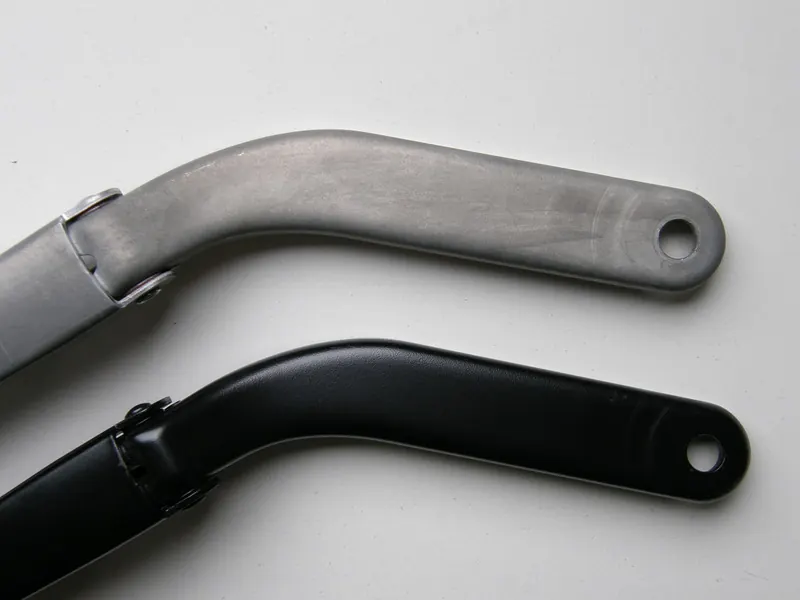
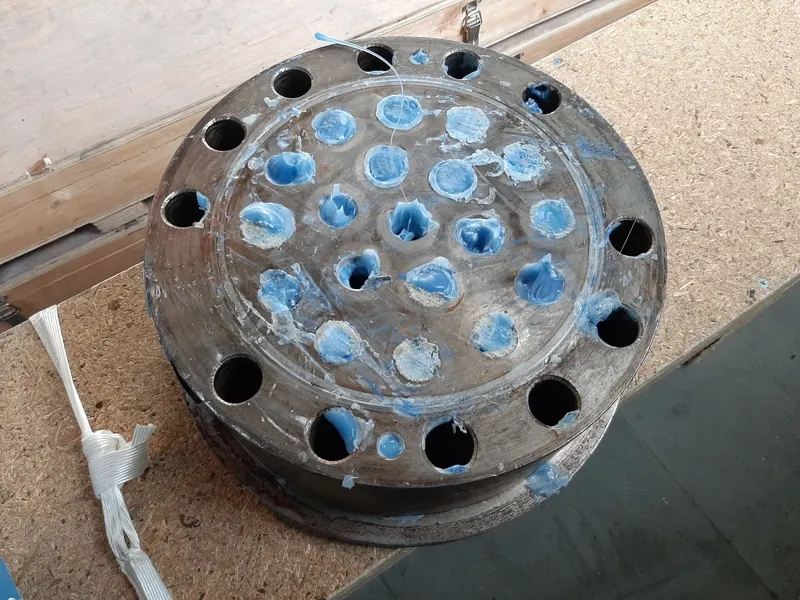
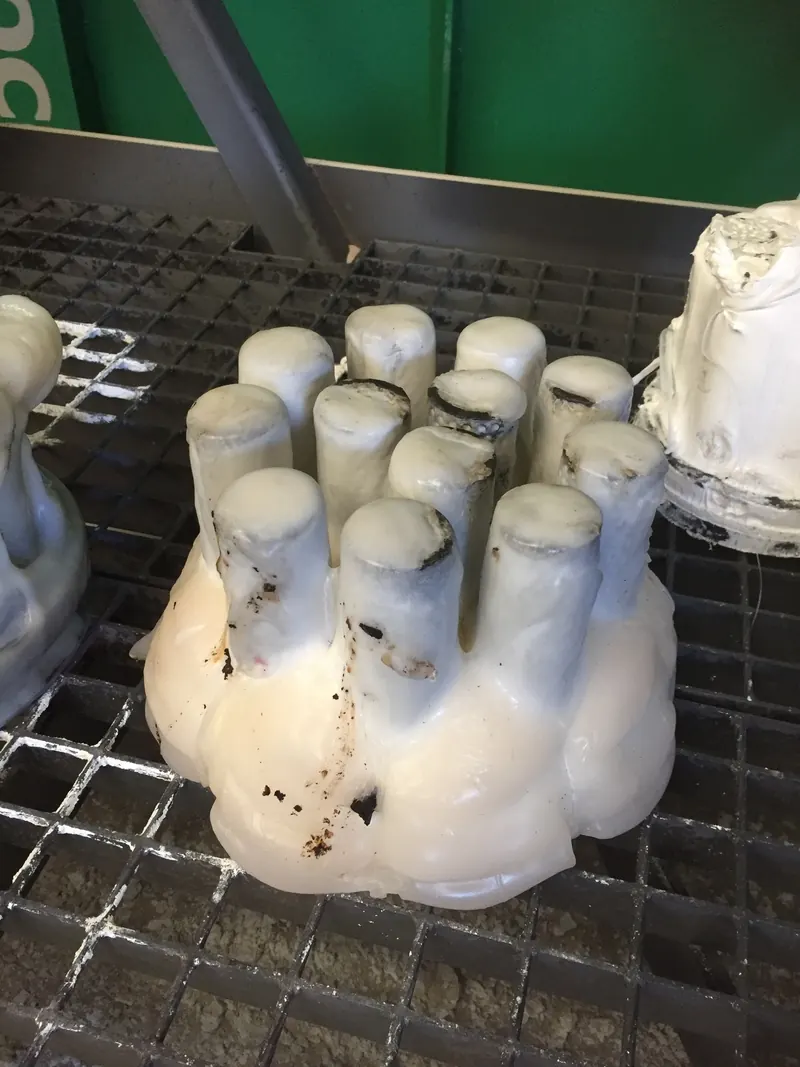
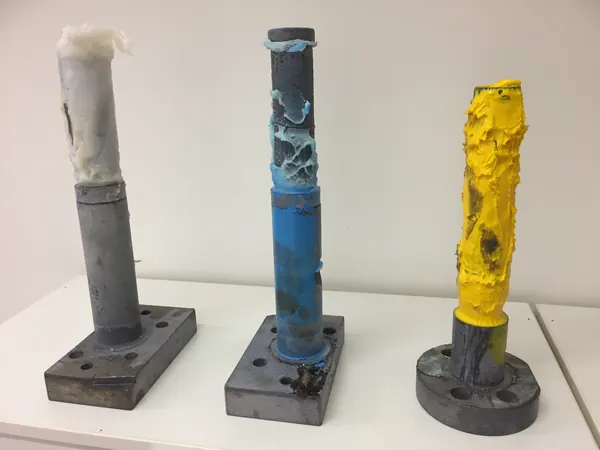
Photos: Arena Comet UK and Arena Comet group.
How pyrolysis cleaning works
Scraping, torching or hard blasting a screw or die costs hours and risks scratched flow surfaces and damaged edges. Pyrolysis removes the polymer with a controlled thermal cycle instead.
The part is loaded into the oven and heated on a programme chosen for the part and the polymer. The bulk of the plastic melts and drains off.
With little oxygen in the chamber, the remaining polymer breaks down into gases instead of burning on the part. The gases are destroyed in an afterburner.
A final controlled stage removes the carbon left behind, leaving only a light, loose ash on the metal.
Ash and inorganic fillers are rinsed or blown off, the part is cooled slowly, checked and prepared for return.
Sectors
Written for maintenance and engineering managers at UK plastics processors and coating lines.
Pipe heads, profile dies, extruder screws and breaker plates.
Flat dies, blown film dies, feedblocks and melt filters from cast and blown film lines.
Spinnerets, spin packs, spin beam parts and filter candles.
Screen changer plates, melt filters, die plates and screw elements from contaminated feedstock.
Crossheads, tips and dies from cable insulation and sheathing lines.
Paint racks, jigs, hooks and hangers from powder coating and wet paint lines.
Why Arena Comet UK
5m × 2m × 2m
Long extruder screws, wide sheet and film dies, spin beams, large melt filters and full paint racks fit in one piece. No cutting, splitting or partial cleaning.
Parkhouse Industrial Estate, Newcastle-under-Lyme, near Stoke-on-Trent, with quick access to the M6 via the A500. Well placed for the Midlands and the North West.
A team that cleans industrial parts every day and knows how polymers, coatings and tooling behave in the oven.
Arena Comet designs and builds thermal cleaning equipment and runs cleaning centres in Belgium, the UK, France, Poland and the Czech Republic.
Your enquiry is handled by a technical sales partner who knows the oven and the site, and who speaks the language of extrusion and maintenance.
From enquiry to clean part
Photo, dimensions, weight and polymer via the form below.
You receive a price and lead time for the cleaning.
Drop off in Newcastle-under-Lyme or we arrange collection.
Pyrolysis cycle programmed for your part and polymer.
Ash removed and the part checked before release.
Packed and returned, ready for your next run.
FAQ
Pyrolysis cleaning removes polymer and other organic residue from metal parts with heat. In a controlled oven the plastic melts off and is broken down into gases, which are burned in an afterburner. A final controlled stage removes the remaining carbon, leaving a light ash that is rinsed or blown off. No scraping, cutting or aggressive blasting is needed to get the polymer off.
The Santana pyrolysis oven at Arena Comet UK has a chamber of 5 m × 2 m × 2 m. Long extruder screws, wide sheet and film dies, spin beams, large melt filters and paint racks can usually be cleaned in one piece. Send the dimensions and weight and we will confirm before you ship.
Most common thermoplastics, such as PE, PP, PS, PET and PA, plus paints and powder coatings. Always tell us the polymer and any additives or fillers: some materials, for example PVC or fluoropolymers, need to be discussed before cleaning.
The cycle runs on a controlled temperature programme chosen for the part and the polymer, which is why pyrolysis is widely used for precision extrusion tooling. Tell us the steel, any surface treatment (nitrided, chrome-plated, bimetallic) and any non-metal components, and we will confirm the right programme before we start.
It depends on the size of the part, the amount of polymer and the load in the oven. You receive a lead time together with the quote.
Yes, collection and return can be arranged. The site is in Newcastle-under-Lyme, Staffordshire, with quick access to the M6 via the A500, so you can also drop parts off yourself during opening hours.
Yes. Paint and powder coating build-up on racks, jigs, hooks and hangers is removed in the same pyrolysis oven, so they make proper electrical contact again.
This website is operated by TuneItUp BV as official sales partner of Arena Comet UK Ltd. All cleaning work is carried out by Arena Comet UK Ltd at Unit 59 Brick Kiln Lane, Parkhouse Industrial Estate West, Newcastle-under-Lyme ST5 7AS.
Request a quote
The more we know, the faster and more accurate the quote: overall dimensions, weight, the polymer or coating, and how much build-up there is.
Opening hours: Mon–Fri, 08:00–16:00
Enquiries via this website are handled by TuneItUp BV, official sales partner of Arena Comet UK Ltd.